Ball Valve vs Globe Valve: Key Differences and Applications
By:Admin
In the rapidly evolving industrial sector, the role of reliable and efficient valve technology cannot be overstated. Among the diverse range of valves available, ball valves and globe valves stand out for their critical applications in controlling fluid flow with precision and durability. Recent advancements and industry insights highlight how these valve types are driving improvements across various industries including oil and gas, water treatment, chemical processing, and power generation.
### Understanding Ball Valves and Globe Valves
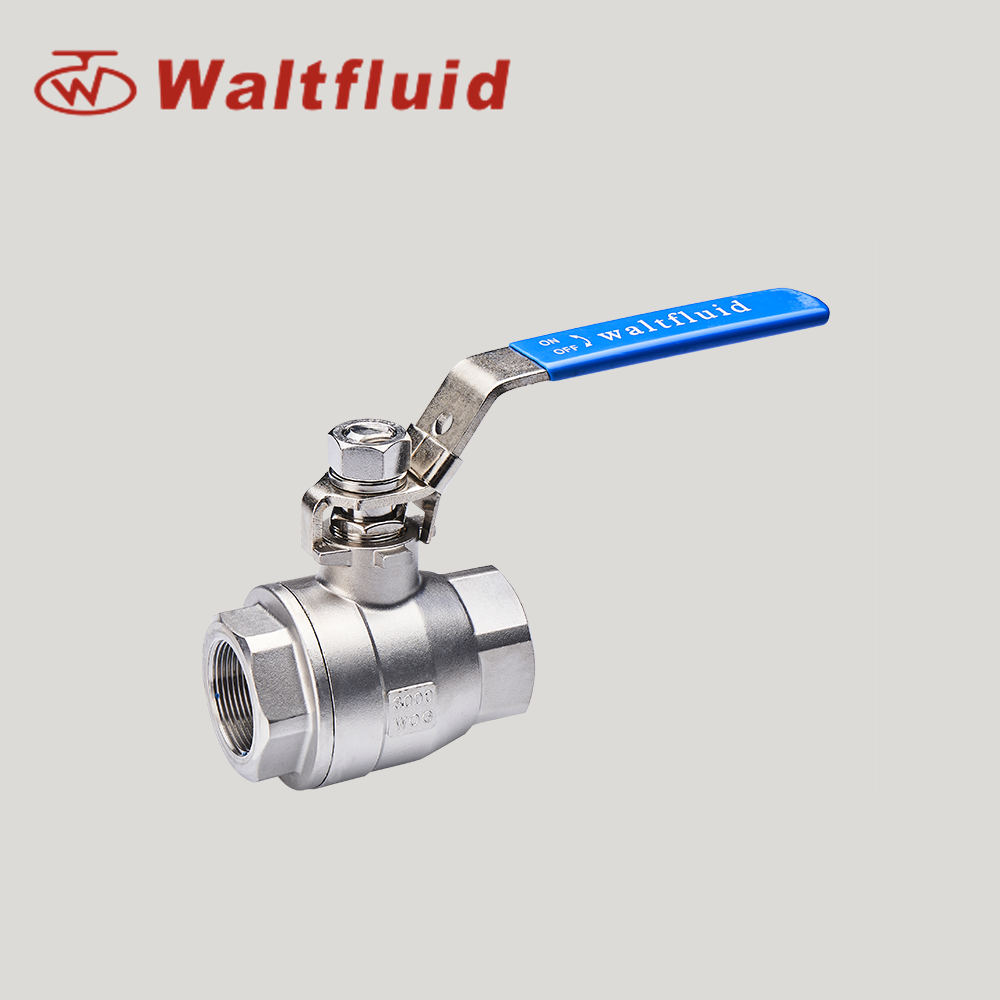
Ball valves are known for their robust design and simple operation. Featuring a spherical disc that controls flow through a hollow, perforated, and pivoting ball, ball valves provide quick on/off control with minimal pressure drop. Their versatility makes them ideal for applications requiring tight shut-off and efficient fluid handling. Additionally, ball valves are valued for their durability and low maintenance, capable of withstanding high pressure, high temperature, and corrosive environments.
Globe valves, on the other hand, offer precise throttling and flow regulation. Characterized by a movable disc-type element and a stationary ring seat inside a spherical body, globe valves excel in handling variable flow conditions and pressure drops. Their design enables better control over flow rate, making them suitable for systems requiring fine adjustments such as steam regulation and cooling water systems.
### Recent Industry Developments
Recent reports from industry experts emphasize significant enhancements in both ball valve and globe valve technologies. Developments in materials science have led to the introduction of advanced alloys and composites, increasing valves’ resistance to corrosion, temperature extremes, and mechanical wear. These improvements extend the operational lifespan and reliability of valves deployed in challenging industrial environments.
Furthermore, precision engineering and automation integration have revolutionized valve performance. Modern ball and globe valves frequently incorporate smart actuators and digital positioners, allowing remote operation, real-time monitoring, and predictive maintenance. Such features minimize downtime and improve operational safety while ensuring compliance with increasingly stringent industry standards.
### Applications and Benefits Across Industries
The versatility of ball valves is evident in sectors like oil and gas, where high-pressure flow control and rapid shutdown capabilities are essential. Similarly, globe valves are extensively utilized in power plants and chemical processing facilities where flow regulation and pressure management are critical for process optimization and safety.
Water treatment and distribution systems also benefit immensely from these valve technologies. Ball valves facilitate efficient isolation of pipeline sections for maintenance, whereas globe valves ensure accurate control of water flow and pressure, contributing to stable and sustainable operations.
### Commitment to Quality and Innovation
Companies specializing in valve manufacturing are committed to continuous innovation, quality assurance, and customer satisfaction. Leveraging state-of-the-art production facilities and rigorous testing protocols, manufacturers deliver valves that meet international standards including ANSI, API, and ISO certifications. Comprehensive after-sales service and technical support further ensure that clients receive reliable solutions tailored to their specific operational needs.
### Conclusion
As industries worldwide confront increasing demands for efficiency, safety, and environmental compliance, the importance of advanced valve technology is more pronounced than ever. Ball valves and globe valves, through ongoing innovation and smart integration, continue to provide indispensable solutions that enhance control, reduce operational risks, and optimize system performance. Stakeholders looking to upgrade their infrastructure or improve process control would benefit from considering these versatile and dependable valve options.
Company News & Blog
Spring Loaded Valve: Key Features and Applications Explained
Certainly! Please provide the company introduction and the news content regarding the Spring Loaded Valve, so I can draft the 800-word news article for you.
The Benefits of Using a High Pressure 3 Way Ball Valve
High Pressure 3 Way Ball Valve: The Latest Innovation in Valve TechnologyWith the ever-increasing demand for reliable and efficient valve solutions, [Company Name] has announced the launch of their high pressure 3 way ball valve. This innovative new product is designed to meet the needs of industries requiring robust and high-performance valve solutions.[Company Name] is a leading supplier of industrial valves, serving a wide range of industries including oil and gas, petrochemical, chemical, and power generation. With a strong focus on innovation and quality, the company has built a solid reputation for providing high-quality valve solutions to meet the most demanding requirements of its customers.The high pressure 3 way ball valve is the latest addition to [Company Name]’s extensive product range. Designed to handle high pressure applications, this valve is built to withstand the most challenging operating conditions. Its rugged construction and durable materials make it the ideal choice for applications where reliability and performance are critical.One of the key features of the high pressure 3 way ball valve is its versatile design, which allows it to be used for a wide range of flow control applications. Whether it's diverting, mixing, or shutting off flow, this valve offers exceptional flexibility and performance. Its compact design also saves space and makes installation and maintenance easier, further enhancing its appeal to customers.In addition to its robust construction and versatile design, the high pressure 3 way ball valve also boasts superior performance characteristics. With its tight shut-off capability, the valve provides excellent flow control and minimizes leakage, ensuring safe and efficient operation. Its smooth, low-torque operation also reduces wear and tear, prolonging the valve’s service life.To ensure the highest level of quality and reliability, [Company Name] has subjected the high pressure 3 way ball valve to rigorous testing and validation. From material selection and manufacturing processes to final testing, the valve undergoes strict quality controls at every stage of production. This commitment to quality and performance is reflected in the valve’s compliance with international standards and industry regulations.The launch of the high pressure 3 way ball valve is a testament to [Company Name]’s ongoing commitment to innovation and customer satisfaction. By understanding the needs and challenges of their customers, the company continues to develop and introduce cutting-edge valve solutions that deliver exceptional value and performance.Commenting on the launch of the high pressure 3 way ball valve, [Company Name]’s spokesperson stated, “We are excited to introduce this new addition to our product line. The high pressure 3 way ball valve represents the latest in valve technology and reinforces our commitment to providing our customers with the best solutions for their applications. We are confident that this valve will meet and exceed the expectations of our customers, and we look forward to the positive impact it will have in the industries we serve.”In conclusion, the launch of the high pressure 3 way ball valve by [Company Name] represents a significant milestone in the field of valve technology. With its robust construction, versatile design, and superior performance, this valve is poised to set new standards in high-pressure flow control applications. As industries continue to demand reliable and efficient valve solutions, [Company Name] remains at the forefront, delivering innovative and high-quality products to meet the evolving needs of its customers.
High-Quality and Reliable Knife Edge Gate Valve for Industrial Use
Knife Edge Gate Valve Market to Witness Robust Expansion by 2027The global Knife Edge Gate Valve market is expected to expand at a significant rate in the coming years, according to a new report by [Company Name]. The market is anticipated to grow at a CAGR of over 5% from 2020 to 2027. The increasing demand for Knife Edge Gate Valves in various industries, such as oil and gas, wastewater treatment, chemical, and power generation, is driving the market growth.Knife Edge Gate Valves are designed to handle tough applications, such as slurries, powders, and granules, where traditional valves may fail. These valves are widely used in industries where abrasive and viscous media flow, due to their ability to prevent clogging and provide a tight shut-off. The rising need for efficient and reliable valves in industrial processes is boosting the demand for Knife Edge Gate Valves.[Company Name] is a leading manufacturer of Knife Edge Gate Valves, offering a wide range of products that cater to the diverse requirements of different industries. The company's valves are known for their high performance, durability, and low maintenance, making them a preferred choice for many customers worldwide.The Knife Edge Gate Valve market is witnessing significant growth, driven by the increasing investments in industrial infrastructure and the expansion of end-use industries. The growing demand for water and wastewater treatment plants, coupled with the rising focus on environmental protection, is driving the adoption of Knife Edge Gate Valves in the global market. Additionally, the expansion of the oil and gas industry and the increasing exploration and production activities are likely to contribute to the market growth.[Company Name] is focused on continuously improving its product offerings to meet the evolving needs of its customers. The company's commitment to innovation and quality has made it a trusted partner for many leading companies across the world. With a strong presence in key markets and a widespread distribution network, [Company Name] is well-positioned to capitalize on the growing demand for Knife Edge Gate Valves.The recent advancements in technology have also played a significant role in the growth of the Knife Edge Gate Valve market. The integration of advanced materials and design innovations has led to the development of more efficient and reliable valves, further fueling the market growth. [Company Name] has been at the forefront of these technological advancements, leveraging its expertise to deliver cutting-edge solutions to its customers.Geographically, the Asia Pacific region is poised to witness substantial growth in the Knife Edge Gate Valve market, driven by the expansion of industrial infrastructure and the rapid industrialization in countries like China and India. The increasing investments in infrastructure development, coupled with the growing focus on enhancing operational efficiency, are expected to propel the demand for Knife Edge Gate Valves in the region.In conclusion, the global Knife Edge Gate Valve market is on a trajectory of steady growth, driven by the increasing demand from various industries and the ongoing technological advancements. With its robust product portfolio, commitment to quality, and extensive market reach, [Company Name] is well-positioned to capitalize on the opportunities presented by this growing market. As the company continues to innovate and expand its presence in key regions, it is poised to emerge as a leading player in the global Knife Edge Gate Valve market.
Top Trunnion Mounted Ball Valve Manufacturers in China
**China Trunnion Mounted Ball Valve Manufacturers: Industry Overview and Market Dynamics**In recent years, China has firmly established itself as a global hub for the manufacturing of high-quality industrial valves, particularly trunnion mounted ball valves. These valves, known for their durability, reliability, and efficient operational characteristics, are pivotal components across various industries including oil and gas, petrochemical, power generation, and water treatment sectors. As market demand escalates both domestically and internationally, Chinese manufacturers continue to innovate and expand production capabilities to meet diverse client requirements.### Industry Landscape and Market DemandTrunnion mounted ball valves are engineered to offer enhanced sealing performance and reduced operating torque compared to floating ball valves. Their design includes a shaft fixed to a ball that is supported on both ends, providing superior stability and reliability under high-pressure conditions. This makes them highly suitable for large-diameter pipelines and systems handling high-pressure fluids.China’s valve manufacturing sector benefits from advanced industrial infrastructure, skilled labor, and ongoing investment in research and development. Over the past decade, the country has seen accelerated modernization of its production facilities, incorporating precision machining, automated assembly lines, and stringent quality control measures aligned with international standards such as API 6D and ISO 9001. These advancements have significantly improved product quality, enabling Chinese manufacturers to compete effectively against established global valve producers.### Key Technological AdvancesChinese manufacturers have focused on integrating cutting-edge technology to enhance the functionality and longevity of trunnion mounted ball valves. Innovations include the use of corrosion-resistant alloys, advanced seat materials designed for extended wear resistance, and enhanced sealing technologies to prevent leakage even under extreme conditions. Additionally, enhancements in actuation systems—such as electric, pneumatic, and hydraulic actuators—have made valve operation more efficient and automated, reducing maintenance costs and improving safety.Smart valve technology also represents a growing trend within the industry, with manufacturers developing valves equipped with sensors for real-time monitoring of parameters including temperature, pressure, and valve position. This digital integration facilitates predictive maintenance and reduces downtime in critical applications—factors highly valued by clients in energy and chemical industries.### Market Expansion and Export GrowthChina’s trunnion mounted ball valve manufacturers have expanded their footprint across global markets, fueled by competitive pricing, consistent product quality, and compliance with international standards. Economic growth in emerging markets, particularly across Asia, Africa, and Latin America, has led to increased infrastructure development projects requiring reliable valve solutions. Chinese firms are leveraging this demand, translating into a surge in exports and strategic overseas partnerships.Furthermore, domestic initiatives such as the Belt and Road Initiative (BRI) have opened up numerous opportunities for pipeline and infrastructure projects, increasing local demand for advanced valve technologies. Chinese manufacturers are actively collaborating with engineering, procurement, and construction (EPC) companies to provide customized valve solutions tailored to specific geographic and industrial needs.### Sustainability and Environmental ConsiderationsAlongside technological progress, there is growing emphasis on sustainability within China’s valve manufacturing sector. Manufacturers are adopting eco-friendly production processes to reduce carbon footprint and waste generation. Material selection prioritizes recyclable and environmentally benign components, while energy-efficient manufacturing techniques minimize resource consumption.In response to international environmental regulations and client expectations, the design of trunnion mounted ball valves increasingly incorporates features to prevent fugitive emissions. Sealing systems are optimized to comply with standards such as ISO 15848, making valves suitable for use in environmentally sensitive applications such as gas processing and chemical manufacturing. This not only enhances the environmental credentials of Chinese products but also strengthens their appeal in stringent regulatory markets like Europe and North America.### Challenges and Future OutlookDespite notable achievements, Chinese manufacturers of trunnion mounted ball valves face several challenges. Intense global competition necessitates continuous innovation and cost optimization. Additionally, trade tensions and tariff barriers potentially impact export growth. To mitigate these risks, companies are investing in diversification of supply chains and expanding local service networks to better support after-sales requirements.Looking forward, the outlook for China’s trunnion mounted ball valve industry remains positive. Increasing industrialization, infrastructure investments, and energy sector developments foster sustained demand. Technological innovation combined with digital transformation is expected to drive new product offerings and enhanced operational efficiencies. Integration of Industry 4.0 principles—including IoT connectivity, predictive analytics, and automation—will further elevate product capability and customer satisfaction.### ConclusionChina’s trunnion mounted ball valve manufacturers have evolved into significant contributors to the global valve industry landscape. Through continuous technological innovation, adherence to international quality standards, and expansion into emerging markets, they are well-positioned to support the increasing demand for robust, efficient, and environmentally conscious valve solutions worldwide. As the industry embraces digitalization and sustainable practices, China’s manufacturers are set to remain competitive players in the dynamic global marketplace.---*This overview provides insights into the current status and future potential of China’s trunnion mounted ball valve manufacturing sector, underscoring the country’s growing role in supplying critical industrial components to diverse applications worldwide.*
Three Way Ball Valve: Features, Uses, and Advantages
**Innovative Three Way Ball Valve Redefines Flow Control Technology**In an era where industrial efficiency and reliability are paramount, the introduction of the latest Three Way Ball Valve marks a significant advancement in fluid control systems. This valve, designed with cutting-edge technology and engineered for durability, promises to enhance operational flexibility across various industries. Backed by a company renowned for its commitment to quality and innovation, this product is set to become a staple in facilities requiring precise and reliable fluid management.### Revolutionizing Fluid Control with the Three Way Ball ValveThe Three Way Ball Valve is a versatile device engineered to regulate, divert, or combine fluid flows within piping systems efficiently. Unlike traditional two-way valves, this valve features three ports, offering more complex flow control options. This enhanced functionality is particularly beneficial in industries such as chemical processing, water treatment, pharmaceuticals, and oil and gas, where flow paths often need to be re-routed quickly and reliably.One of the standout features of this three-way valve is its ability to switch flow directions seamlessly without interrupting ongoing processes. This functionality significantly reduces downtime and maintenance costs, ensuring smoother operations. The valve's robust design incorporates high-grade materials that withstand extreme temperatures and pressures, providing longevity even in the most demanding environments.### Key Features and Benefits- **Enhanced Flow Control:** The three ports allow for various flow configurations, including mixing, diverting, or selective flow paths, giving operators enhanced control flexibility.- **Durable Construction:** Manufactured using corrosion-resistant alloys, the valve ensures long-term performance and minimizes risks associated with material degradation.- **Ease of Operation:** With an ergonomic handle and automated actuator compatibility, the valve offers both manual and remote operation options, catering to diverse user needs.- **Leak-proof Design:** Advanced sealing technology guarantees minimal leakage, maintaining system integrity and environmental safety.- **Low Maintenance:** Designed with fewer moving parts and easy access for servicing, the valve reduces maintenance downtime and operational costs.### Company Profile: A Legacy of Excellence in Valve ManufacturingThis breakthrough product is developed by a company with decades of experience in engineering high-quality valve solutions. Established with a vision to provide innovation-driven products, the company has consistently invested in research and development to meet the evolving demands of industrial automation and fluid management.Their product portfolio spans a wide range of valves, including ball valves, butterfly valves, check valves, and specialized flow control devices, all tailored to meet stringent industry standards. Equipped with state-of-the-art manufacturing facilities, the company adheres to international certifications such as ISO 9001 and API standards, ensuring that every product delivered meets global quality benchmarks.A strong commitment to customer satisfaction drives the company’s approach to manufacturing and service. Besides providing durable and efficient products, they offer extensive technical support and customized solutions to address specific operational challenges faced by clients worldwide.### Applications Across Diverse IndustriesThe adaptable nature of the Three Way Ball Valve makes it ideal for implementation in multiple sectors:- **Chemical Industry:** Facilitates the diversion and mixing of corrosive fluids, optimizing chemical reactions and processes while ensuring safety.- **Water and Wastewater Treatment:** Enables effective segregation and control of water flow in treatment plants, enhancing purification efficiency.- **Pharmaceutical Manufacturing:** Supports sterile and controlled fluid pathways necessary for drug formulation and processing.- **Oil and Gas:** Permits efficient distribution and shutdown operations in pipelines, reducing the risk of spills and downtime.In each of these sectors, the valve’s reliability and precision contribute to increased productivity and reduced operational risks.### Commitment to Sustainability and InnovationBeyond product excellence, the company prioritizes environmental responsibility. The design of the Three Way Ball Valve incorporates eco-friendly manufacturing processes and materials that reduce waste and energy consumption. This focus aligns with global efforts to reduce industrial environmental footprints.Further, ongoing innovation ensures that the valve series continues to evolve, integrating smart technology options such as IoT-enabled actuators for remote monitoring and control. This advancement empowers facility managers with real-time data analytics, predictive maintenance capabilities, and enhanced system integration.### Customer Success StoriesSeveral industry leaders have already integrated the Three Way Ball Valve into their operations, reporting significant improvements in system efficiency and reliability. For instance, a major chemical processing plant noted a 20% reduction in downtime after replacing traditional valves with the new three-way design. Similarly, a water treatment facility highlighted enhanced control over flow management, which directly improved water quality outcomes.### Looking AheadAs industries continue to seek solutions that combine performance, reliability, and cost-effectiveness, this Three Way Ball Valve stands out as a definitive choice. Supported by a company with a proven track record and commitment to innovation, the valve is poised to meet the increasing complexity and demand of modern industrial fluid control systems.For businesses aiming to enhance their operational capabilities, adopting this advanced valve technology represents a forward-thinking investment that promises tangible benefits in efficiency, safety, and sustainability.---For more information about the Three Way Ball Valve and tailored solutions for your industry needs, please contact the company’s representatives or visit their website.
6 Flanged Check Valves: A Comprehensive Guide
, with 6 Check Valve Flanged at the center of the story, here's a possible 800-word news piece:Flanged Check Valves Ensure Efficient and Safe Flow ControlIn the realm of fluid and gas control, one cannot overemphasize the importance of reliable and efficient check valves. And when it comes to high-quality check valves, one company that stands out is {}.With a rich history of providing top-notch fluid control solutions to a wide array of industries, {} has continually proven its commitment to quality, innovation, and customer satisfaction. As a leading manufacturer and supplier of industrial valves, {} has gained a reputation for delivering products that meet the highest standards of performance and reliability.One of the standout products from the company's extensive valve portfolio is the Flanged Check Valve. Engineered with precision and designed to meet the diverse needs of modern fluid and gas control systems, {}'s Flanged Check Valve offers a combination of robust construction, efficient performance, and long-term reliability.The Flanged Check Valve is specifically designed to prevent backflow and ensure unidirectional flow of fluids and gases in pipelines. This feature makes it an indispensable component in a variety of applications, including water treatment, oil and gas, petrochemical, pharmaceutical, and power generation industries.What sets {}'s Flanged Check Valve apart from others in the market is its superior build quality and advanced design. Constructed from high-grade materials such as stainless steel, carbon steel, and alloy steel, these valves exhibit exceptional corrosion resistance and durability, making them suitable for use in demanding industrial environments.Moreover, the Flanged Check Valves are available in a wide range of sizes, pressure ratings, and end connections, allowing for seamless integration into different piping systems. This flexibility, combined with the valves' easy installation and maintenance, makes them a cost-effective and practical solution for fluid control applications.The Flanged Check Valves from {} are also designed to meet international standards for quality and performance. Rigorously tested and certified to ensure compliance with industry regulations, these valves provide users with the assurance of safe and reliable operation.In addition to their technical prowess, {}'s Flanged Check Valves are backed by the company's commitment to customer support and service. With a dedicated team of experts and a global network of distributors, {} ensures that its customers receive prompt assistance, technical guidance, and timely delivery of products.As a result, customers can rely on {}'s Flanged Check Valves for efficient and trouble-free operation, contributing to increased productivity and reduced downtime in their operations.With a track record of successful installations and satisfied customers worldwide, {}'s Flanged Check Valves have earned a reputation for excellence in flow control. Whether it's preventing reverse flow in water distribution systems or maintaining pressure in chemical processing plants, these valves deliver consistent performance and peace of mind to their users.In conclusion, {}'s Flanged Check Valves represent the epitome of quality, reliability, and performance in fluid and gas control. With their advanced design, robust construction, and global support, these valves are a testament to {}'s commitment to providing cutting-edge solutions for the evolving needs of industrial applications.For businesses and operations seeking dependable check valves for their fluid and gas control systems, {}'s Flanged Check Valves offer a compelling choice that ensures efficient and safe flow control.
4-Way Valve Factory: Everything You Need to Know
The 4 Way Valve factory, located in the heart of a bustling industrial district, is a key player in the production of high-quality valves for various industries. Its state-of-the-art facilities and advanced technology have made it a leader in the valve manufacturing industry, providing reliable and efficient products to customers around the world.Established over 30 years ago, the factory has continuously evolved and expanded its capabilities to meet the growing demands of the market. With a strong focus on research and development, the company has been able to innovate and create cutting-edge solutions that cater to the specific needs of its clients.The 4 Way Valve factory is committed to adhering to the highest quality standards in every aspect of its operations. From sourcing the finest raw materials to employing skilled technicians and engineers, the company ensures that every product that leaves its facilities meets the strictest quality control measures.One of the key products manufactured at the 4 Way Valve factory is the 4 way valve, a crucial component in various industrial applications. These valves are designed to control the flow of liquids and gases in different directions, providing a versatile and efficient solution for a wide range of systems.The manufacturing process of the 4 way valve involves precision engineering and meticulous attention to detail. Each valve is crafted with precision and accuracy to ensure flawless performance and maximum durability. With a focus on meeting the unique specifications of its clients, the factory is able to customize the valves to suit specific applications, making them a preferred choice for many industries.In addition to manufacturing, the 4 Way Valve factory also places a strong emphasis on sustainability and environmental responsibility. The company is mindful of its impact on the environment and takes proactive measures to minimize its carbon footprint. Through the use of energy-efficient practices, waste reduction initiatives, and eco-friendly materials, the factory strives to operate in an environmentally sustainable manner.Furthermore, the factory takes pride in its commitment to workplace safety and employee well-being. Stringent safety protocols and regular training programs ensure that the workforce is equipped with the knowledge and skills to operate in a safe and secure environment. This dedication to safety not only protects the employees but also upholds the reputation of the company as a responsible and ethical manufacturer.The 4 Way Valve factory also believes in giving back to the community and actively participates in various social initiatives and charity programs. By supporting local causes and contributing to the welfare of the community, the factory strives to make a positive impact beyond its business operations.As the demand for high-quality valves continues to grow, the 4 Way Valve factory remains poised to meet the needs of its customers with its unwavering commitment to excellence. With a focus on innovation, quality, sustainability, and social responsibility, the company is well-positioned to maintain its leading position in the industry and continue serving its clientele with exceptional products and services.In conclusion, the 4 Way Valve factory stands as a shining example of a company that not only excels in its business endeavors but also upholds strong values in every aspect of its operations. With its dedication to quality, sustainability, and social responsibility, the factory is a beacon of success in the manufacturing industry. As it continues to innovate and adapt to the evolving market, the 4 Way Valve factory is poised to remain a top choice for customers seeking reliable and high-performance valve solutions.
Durable Knife Gate Slurry Valves for Efficient Industrial Use
Knife Gate Slurry Valves: The Perfect Solution for Abrasive Material HandlingIn the world of industrial processes, handling abrasive and corrosive materials can be a significant challenge. Whether it's in mining, wastewater treatment, or power generation, the need for reliable and efficient valves to control the flow of such materials is crucial. This is where Knife Gate Slurry Valves come into play, offering a perfect solution for the handling of abrasive materials in various industries.In recent years, (company name) has emerged as a leading manufacturer and supplier of high-quality Knife Gate Slurry Valves. With a strong focus on innovation and product development, (company name) has been able to provide its customers with reliable and efficient valve solutions that meet their specific needs and requirements.One of the key features of Knife Gate Slurry Valves is their ability to handle abrasive and corrosive materials with ease. This is achieved through the use of high-quality materials and advanced design principles that ensure the valves can withstand the harsh conditions they are often exposed to. The valves are also designed to provide a tight shut-off, preventing any leakage of the abrasive material being handled.Another important feature of Knife Gate Slurry Valves is their versatility. They can be used in a wide range of applications, including mining, mineral processing, wastewater treatment, and power generation. This versatility makes them an ideal choice for industries that regularly deal with abrasive materials and require reliable valve solutions.In addition to their durability and versatility, Knife Gate Slurry Valves are also known for their ease of maintenance. With a simple and straightforward design, these valves can be easily accessed and serviced, reducing downtime and ensuring the continuous operation of the industrial processes they are a part of.Moreover, (company name) takes pride in its commitment to quality and customer satisfaction. The company's team of highly skilled engineers and technicians work tirelessly to ensure that every valve is manufactured to the highest standards and meets the specific requirements of its customers. This dedication to quality has earned (company name) a solid reputation in the industry, making them a trusted partner for businesses looking for reliable valve solutions.One of the key factors that set (company name) apart from its competitors is its focus on innovation. The company continually invests in research and development to improve its products and develop new solutions that meet the ever-evolving needs of its customers. This commitment to innovation has led to the development of advanced features and technologies that make Knife Gate Slurry Valves stand out in terms of performance and reliability.In conclusion, Knife Gate Slurry Valves offered by (company name) provide the perfect solution for industries that require reliable and efficient valve solutions for handling abrasive and corrosive materials. With a strong focus on quality, innovation, and customer satisfaction, (company name) has established itself as a leading provider of high-quality Knife Gate Slurry Valves that meet the diverse needs of its customers. Whether it's in mining, mineral processing, wastewater treatment, or power generation, businesses can rely on (company name) to provide them with the perfect valve solutions for handling abrasive materials.
Top Wholesale 3 Way Ball Valve Factories for Pex Plumbing Systems
Wholesale Pex 3 Way Ball Valve Factories has recently seen a surge in demand for their products, prompting them to further ramp up their production to meet the needs of their customers. The company, which specializes in manufacturing high-quality ball valves, has been a leading player in the industry for several years. With their state-of-the-art facilities and a commitment to excellence, they have established themselves as a trusted supplier in the market.The company's success can be attributed to their dedication to producing top-notch products that meet the highest standards of quality and performance. Their Pex 3 Way Ball Valves are designed to deliver reliable and efficient operation, making them an ideal choice for a wide range of applications. Whether it's for residential, commercial, or industrial use, Wholesale Pex 3 Way Ball Valve Factories' products are known for their durability, longevity, and outstanding performance.In addition to their commitment to quality, the company also prides itself on providing exceptional customer service. They understand the importance of meeting their clients' needs and strive to offer personalized solutions that cater to specific requirements. This approach has earned them a loyal customer base, as well as a solid reputation for being a dependable and customer-focused supplier.As part of their expansion plans, Wholesale Pex 3 Way Ball Valve Factories has been investing in advanced technologies and equipment to increase their production capacity. By modernizing their manufacturing processes, they aim to streamline operations and meet the growing demand for their products. This investment underscores their commitment to staying ahead of the curve and maintaining their position as an industry leader.Furthermore, the company is constantly exploring new opportunities to expand their market reach and forge partnerships with distributors and retailers. By collaborating with other businesses, they seek to broaden their distribution network and make their products more accessible to customers across different regions. This proactive approach reflects their ambition to grow their business and maximize their impact in the industry.In line with their commitment to sustainability, Wholesale Pex 3 Way Ball Valve Factories also prioritizes environmental responsibility in their operations. They are dedicated to minimizing their ecological footprint and implementing eco-friendly practices that align with their values. This dedication to sustainability sets them apart as a conscientious and forward-thinking manufacturer in the industry.Looking ahead, Wholesale Pex 3 Way Ball Valve Factories is poised to continue its growth trajectory and uphold its reputation as a premier provider of high-quality ball valves. By staying true to their core values of excellence, innovation, and customer satisfaction, they are well-positioned to capture new opportunities and overcome challenges in the market.In conclusion, Wholesale Pex 3 Way Ball Valve Factories has emerged as a standout player in the industry, thanks to their unwavering commitment to quality, customer service, and innovation. With their focus on expansion and sustainability, they are setting the stage for continued success and are poised to make a lasting impact in the market. As they continue to push the boundaries of excellence, they are sure to solidify their position as a top choice for customers seeking superior Pex 3 Way Ball Valves.
3 Way Gate Valve: Features, Applications, and Benefits
Certainly! Please provide the company introduction and any specific key points or details from the news content about the 3 Way Gate Valve that you'd like me to include. Once I have that information, I can draft the 800-word news article for you.